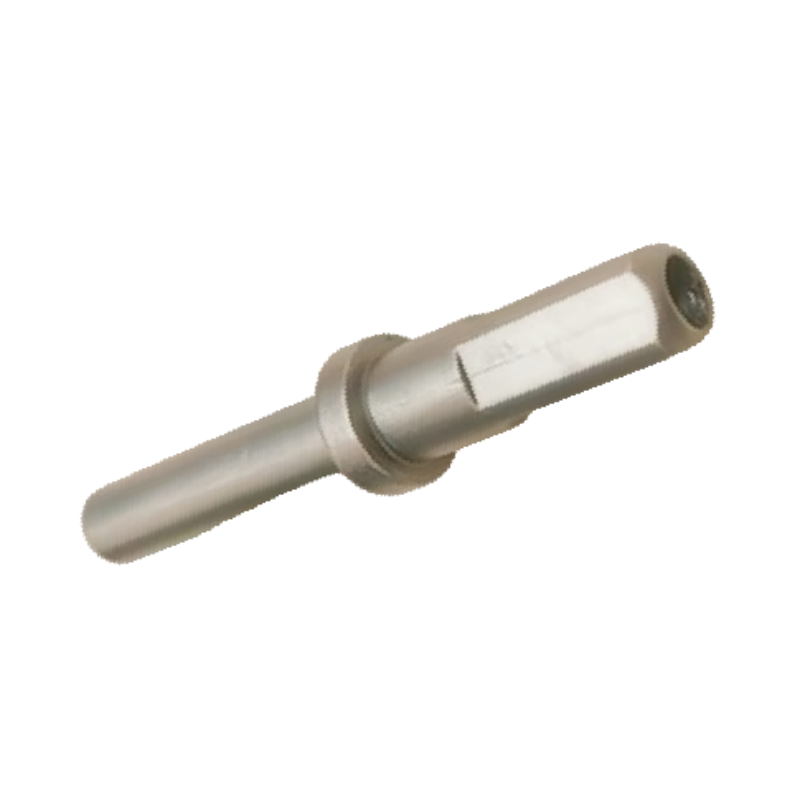
Parameter / Process |
Specification & Technical Highlights |
Customer Benefits / Value |
Material |
Grade 304 Stainless Steel (CF8 / 1.4308 Premium Standard) |
Guarantees excellent oxidation protection, strict sanitation/cleanliness standards for appliances, and long-term rust-free electrical safety. |
Application Scenario |
Electrical Appliances / Precision Instruments / Smart Home Hardware Systems |
Perfect for highly delicate fluid pathways, miniature heater sleeves, sensor probe housings, and micro-conduits. |
Ultra-Light Weight |
0.0406 kg (40.6g Micro-Precision Profile) |
Showcases extreme lightweight accuracy and uniform thin-wall structural execution. |
Internal Cavity |
Slender Through-Hole Architecture |
Executes high length-to-diameter ratios flawlessly; smooth internal bore ensures frictionless fluid transition or wire routing. |
Coring Technology |
Advanced Ceramic Core Inlay Method |
Pre-formed rigid ceramic cores prevent mold deformation; removes operational complexity and ensures perfect internal bore dimensions. |
Production Matrix |
Shortened Manufacturing Cycle & Enhanced Yield Rate |
Optimized lean workflow reduces manual shell-making hours, delivering faster lead times and lower defect overheads. |
Casting Tolerance |
ISO 8062 (GB/T6414) CT6 Grade |
Elite micron-level geometric dimensional repeatability for miniature, mass-produced electronics-grade components. |
Miniature appliance hardware leaves zero margin for geometric shifting or internal roughness. Our laboratory runs an advanced testing suite:
This pivot is presented as a representative custom‑manufactured component for Electrical appliances; Precision instruments; Smart‑home hardware systems; Fluid pathways, miniature heater sleeves, sensor probe housings and micro‑conduits Honyang Cast develops similar parts from customer drawings rather than offering a fixed catalog specification.
The manufacturing plan must connect the part's functional geometry—Slender through‑hole architecture; High length‑to‑diameter internal bore—with tooling, investment casting, machining and measurable inspection requirements. Final dimensions, interfaces and acceptance criteria are confirmed during drawing review.
PROJECT‑SPECIFIC SUPPLY
Material grade, dimensions, tolerance zones, machining allowance, surface condition, operating requirements and inspection records are confirmed after review of the customer’s 2D drawing, 3D model and project specification.
The parameter set is selected for this component’s function. Unknown values remain drawing‑controlled and must not be replaced with generic catalog data.
| Engineering Item | Reference / Custom Requirement | Verification Basis |
|---|---|---|
| Material grade | Grade 304 Stainless Steel (CF8 / 1.4308 Premium Standard) | Confirm governing standard and chemistry requirements. |
| Part weight | 0.0406 kg (40.6 g) | Confirm target weight and allowable variation when relevant. |
| Functional geometry | Slender through‑hole architecture; High length‑to‑diameter internal bore | Identify drawing datums and critical‑to‑function features. |
| Casting / process reference | Advanced ceramic‑core inlay method; Page states a shortened manufacturing cycle and enhanced yield rate | Confirm which steps apply to the quoted production route. |
| Dimensions and tolerances | To be confirmed from customer drawing. | Define casting tolerance separately from machined dimensions and GD&T. |
| Operating conditions | To be specified by customer. | Provide medium, load, temperature, pressure, speed or hygiene requirements as applicable. |
| Recommended additional fields | Add verified title, bore dimensions, wall thickness, envelope size and datum tolerances. | Complete before publishing numeric claims or quoting production. |
| Structural Feature | Why It Matters | Manufacturing Response |
|---|---|---|
| Slender through‑hole architecture | This feature influences fit, flow, load transfer, manufacturability or downstream assembly. | Review core strategy, cavity access, local wall thickness and cleanliness verification for the internal or intersecting features. |
| High length‑to‑diameter internal bore | This feature influences fit, flow, load transfer, manufacturability or downstream assembly. | Translate the feature into drawing datums, casting controls, machining scope and measurable inspection characteristics. |

A project‑specific route is established after review of geometry, alloy, tolerance, volume and validation requirements.
Source Page Process References
PROCESS SCOPE
Investment casting and CNC machining are described as the core route. Heat treatment, coating, polishing, balancing, pressure testing, radiographic testing, PPAP or other special processes must be shown as project‑specific unless their scope is confirmed.
Honyang Cast supports drawing‑based development of pivot and related investment cast components from manufacturability review through sample approval and repeat production.
| Application Requirement | Manufacturing Value |
|---|---|
| Drawing‑defined fit and function | A part‑specific DFM and inspection plan links casting geometry to the actual assembly and operating requirement. |
| Integrated complex geometry | Investment casting can consolidate features and reduce fabrication or excessive stock removal where the approved design supports it. |
| Repeatable critical interfaces | Controlled datums, machining and inspection support consistent assembly of functional surfaces and mating features. |
| Material and process traceability | Agreed material and inspection records provide evidence against the drawing and quality plan. |
| Product‑specific value | Clarify whether the part is truly a pivot or a sleeve/conduit component before creating sales copy. |
Design Inputs Required From the Customer
SEND YOUR DRAWING FOR A MANUFACTURABILITY REVIEW
Upload the drawing and 3D model for your pivot together with material, quantity, operating conditions and inspection requirements. Our team will review the casting route, machining scope and quality plan before quotation.

Leading manufacturer specializing in precision investment casting and CNC machining of high-performance steel components for critical industrial applications.
 EN